NEWS

LATEST How to Reduce Energy Consumption in Crushing Plants: 10 Practical Ways to Lower Cost per Ton

Electricity is one of the major operating expenses in many mining and aggregate crushing plants. As energy prices fluctuate and production costs increase, quarry owners and mining operators are paying closer attention to how efficiently their equipment converts electrical energy into finished products.

However, reducing energy consumption is not simply a matter of choosing a crusher with a smaller motor.

A crushing plant is an interconnected system. Feeders, crushers, vibrating screens, conveyors, and auxiliary equipment all consume energy. Poor equipment matching, excessive recirculating loads, unstable feeding, and unnecessary idle operation can increase electricity consumption without producing additional saleable material.

For plant operators, the more useful question is not necessarily how to reduce total electricity use, but how to reduce energy consumption per ton of finished product while maintaining the required capacity and product quality.

This article explains the main factors affecting crushing plant energy consumption and provides ten practical ways to improve energy efficiency and lower production costs.

1. Understand Where Energy Is Consumed in a Crushing Plant

Before making changes, operators need to understand how electricity is used throughout the production line.

In a typical aggregate crushing plant, the major electricity-consuming equipment includes:

  • Primary crushers, such as jaw crushers and gyratory crushers.

  • Secondary and tertiary crushers, including cone crushers and impact crushers.

  • Sand-making machines, particularly in manufactured sand production.

  • Vibrating screens and feeding equipment.

  • Belt conveyors and other material-handling systems.

  • Dust collection, water pumps, and auxiliary equipment.

The proportion of energy consumed by each machine varies considerably depending on the plant configuration, material hardness, reduction ratio, and required final product sizes.

For example, a hard granite crushing plant with several crushing stages may have a different energy profile from a limestone production line using impact crushing.

Similarly, a plant producing fine manufactured sand may require additional size reduction and classification compared with a plant producing only coarse aggregates.

Rather than focusing on one machine, operators should evaluate the electricity consumption of the complete process.

2. Measure Energy Consumption per Ton, Not Just Total Power

One of the most useful indicators of crushing plant efficiency is specific energy consumption.

It measures how much electricity is used to produce one ton of material.

The basic calculation is:

Specific Energy Consumption (kWh/t) = Total Electricity Consumption (kWh) ÷ Total Production (t)

For example, consider two crushing plants processing similar material and producing comparable finished products.

IndicatorPlant APlant B
Electricity consumption4,800 kWh4,500 kWh
Finished production800 tons900 tons
Specific energy consumption6.0 kWh/t5.0 kWh/t

In this illustrative example, Plant B consumes less electricity while producing more finished material. Its specific energy consumption is approximately 16.7% lower.

However, comparisons are only meaningful when the plants process similar materials and produce products of comparable quality and size distribution.

A plant producing fine sand will generally have different energy requirements from one producing coarse crushed stone.

Operators should also distinguish between total crusher throughput and saleable finished production. Material circulating repeatedly through a closed crushing circuit should not be counted as additional finished output.

For cost analysis, electricity consumption should be measured against the actual quantity of acceptable finished product.

3. Choose the Right Crusher for the Material

Crusher selection has a significant influence on energy efficiency.

Different crushing technologies apply different forces to reduce rock size. Their performance depends on the hardness, abrasiveness, feed size, and required product shape.

Jaw Crushers for Primary Crushing

Jaw crushers are widely used for primary crushing of hard and abrasive materials.

Their main function is to reduce large rocks to a size suitable for subsequent processing.

A correctly selected jaw crusher should accommodate the expected feed size and provide sufficient capacity without excessive loading or frequent blockages.

An undersized crusher may become a production bottleneck, while an oversized machine operating far below its intended capacity may not provide the most economical solution.

Cone Crushers for Hard Rock Processing

Cone crushers are commonly used in secondary and tertiary crushing of hard materials such as granite, basalt, and many metal ores.

Their suitability for abrasive rock makes them an important option when designing energy-efficient multi-stage crushing circuits.

However, energy efficiency depends on the chamber configuration, feed distribution, discharge setting, and operating conditions.

Selecting the correct crushing chamber and maintaining suitable feeding conditions can help improve throughput and reduce unnecessary recirculation.

Impact Crushers for Suitable Materials

Impact crushers are often considered for limestone and other materials where impact crushing can provide the required reduction and product shape.

They can simplify certain process arrangements, but their suitability depends on material characteristics and wear requirements.

For highly abrasive materials, wear-part consumption may become a major operating cost even when the electrical energy requirement appears attractive.

Therefore, crusher selection should consider both energy consumption and total cost per ton.

4. Maintain Stable and Continuous Feeding

Unstable feeding is a common cause of inefficient crusher operation.

When material enters the crusher in irregular batches, the machine may alternate between low-load and high-load conditions.

This can reduce average production efficiency and make it difficult to maintain consistent product size.

A properly selected vibrating feeder or other suitable feeding system helps regulate material flow.

For cone crushers, feed distribution and chamber loading should follow the manufacturer's recommendations. Suitable choke-feeding conditions may improve performance in applications where they are specified, but the correct operating approach depends on the crusher design.

Operators should monitor feeder speed, crusher power draw, and material levels where suitable instrumentation is available.

The objective is to maintain a stable operating condition without exceeding the machine's rated limits.

A consistent feed rate also helps downstream conveyors and vibrating screens operate more predictably.

5. Avoid Unnecessary Over-Crushing

Over-crushing occurs when material is reduced beyond the size required for the intended product.

This can increase energy consumption, produce excessive fines, and place additional load on downstream screening or classification equipment.

For example, a plant producing 10–20 mm aggregate does not benefit from converting an unnecessarily large proportion of the material into particles smaller than 5 mm unless those fines also have a suitable market.

Excessive fine production can reduce the yield of higher-value aggregate sizes.

To avoid over-crushing, operators should review:

  • Crusher discharge settings.

  • Crushing chamber selection.

  • The number of crushing stages.

  • Screen aperture sizes.

  • Product size requirements.

  • The proportion of fines generated at each stage.

The aim is to achieve the required product gradation with an appropriate amount of size reduction.

In some cases, modifying the screening arrangement can reduce unnecessary crushing without changing the main crusher.

6. Optimize the Closed-Circuit Crushing System

Closed-circuit crushing is commonly used when tighter control over final particle size is required.

In this arrangement, material discharged from a crusher passes through a vibrating screen. Oversized particles return to the crusher for further reduction, while material meeting the required size specification leaves the circuit.

This can improve product size control, but excessive recirculating loads can increase energy consumption.

If too much material returns to the crusher, the equipment repeatedly processes particles that may not be reduced efficiently under the existing settings.

The result can be higher conveyor loading, greater screen demand, and reduced net finished-product capacity.

To improve closed-circuit performance, operators should evaluate the relationship between crusher discharge setting, screen efficiency, and return material size.

The objective is not to eliminate recirculation entirely. It is to maintain the level of recirculation necessary to meet product specifications without overloading the system.

A process audit can help determine whether the recirculating load is appropriate for the selected equipment and product requirements.

7. Improve Vibrating Screen Efficiency

Vibrating screens consume electricity, but their effect on the energy consumption of the overall plant extends beyond their own motors.

Poor screening efficiency can send material back to the crusher unnecessarily.

For example, if particles that already meet the required product size remain in the oversize stream, they may be returned for another crushing cycle.

This increases the quantity of material handled by the crusher and conveyors without necessarily increasing saleable output.

Screening performance depends on several factors, including:

  • Feed particle-size distribution.

  • Screen aperture and media selection.

  • Screen loading and material distribution.

  • Moisture and clay content.

  • Vibration characteristics.

  • Screen deck configuration.

Improving screening efficiency may reduce unnecessary recirculation and help the plant produce more finished material from the same equipment.

However, changes to screen openings must preserve the required product specifications.

8. Reduce Unnecessary Idle Running

Crushing plants often experience short interruptions caused by material shortages, conveyor problems, equipment inspections, or downstream blockages.

During these periods, some equipment may continue running without processing useful material.

Although individual idle periods may appear insignificant, repeated interruptions can increase electricity consumption per ton over time.

A coordinated control system can help manage equipment operation during production interruptions.

For example, when downstream equipment stops, the upstream feeding system may need to stop automatically to prevent material accumulation.

Restart sequences should follow the equipment manufacturer's requirements and the plant's approved operating procedures.

It is important to distinguish between unnecessary idle operation and equipment that must continue running for lubrication, cooling, clearing, or other technical reasons.

Not every machine should be stopped immediately when material flow is interrupted.

The goal is to eliminate avoidable energy use without compromising equipment reliability or safety.

9. Maintain Crushers and Wear Parts Properly

Equipment condition can influence crushing performance and energy consumption.

Worn crushing surfaces may change the effective chamber geometry, affecting material flow, reduction performance, and product gradation.

Damaged or poorly maintained components can also increase mechanical resistance or create operating instability.

For cone crushers, the condition of the mantle and concave should be monitored according to the manufacturer's inspection and replacement guidelines.

For jaw crushers, jaw plate wear and the condition of the crushing chamber should be evaluated regularly.

Maintenance teams should also inspect bearings, lubrication systems, drive components, and other critical assemblies.

However, replacing wear parts too early can increase maintenance costs without delivering proportional benefits.

A condition-based maintenance approach, supported by operating data and regular inspections, can help balance energy performance, equipment reliability, and replacement expenses.

10. Evaluate the Complete Plant Layout and Conveying System

Energy efficiency depends on more than crushing equipment.

Belt conveyors, feeders, and transfer systems can contribute significantly to the total electricity demand of a large production line.

Unnecessary material handling, excessive transfer points, and poorly matched conveyor capacities may increase operating costs.

During plant design, engineers should consider the distance between equipment, site elevation, available space, and the required material flow.

A well-organized layout can reduce unnecessary conveying distances and simplify maintenance.

Conveyor selection should also match the expected material load. Belt speed, width, drive arrangement, and operating conditions all affect performance.

For existing plants, opportunities for improvement may include better conveyor loading, reduced spillage, improved transfer chutes, and maintenance of mechanical components.

The most economical layout is not necessarily the shortest one. It must also provide suitable access, safe operation, and reliable material handling.

11. Calculate Electricity Cost per Ton

Once energy consumption is measured, it can be translated into production cost.

The basic calculation is:

Electricity Cost per Ton = Specific Energy Consumption (kWh/t) × Electricity Price ($/kWh)

Consider a hypothetical aggregate plant producing 500 tons per hour.

<text weight="medium">Example: Energy efficiency improvement</text>

IndicatorBeforeAfter
Production capacity500 t/h500 t/h
Specific energy consumption5.5 kWh/t4.8 kWh/t
Electricity price$0.12/kWh$0.12/kWh
Electricity cost per ton$0.66$0.576

In this example, the improvement reduces electricity cost by $0.084 per ton.

If the plant operates 10 hours per day for 300 days per year, annual finished production would be 1.5 million tons.

The potential annual electricity savings would be:

1,500,000 tons × $0.084/ton = $126,000 per year

This is an illustrative calculation, not a guaranteed saving. Actual results depend on production conditions, energy tariffs, equipment performance, and whether the improved energy consumption can be maintained.

The example demonstrates why even relatively small improvements in specific energy consumption can have a meaningful financial impact at large production volumes.

12. Should You Replace Old Crushers with More Energy-Efficient Equipment?

Upgrading equipment may improve production efficiency, but replacement should not be the first response to every energy problem.

Before investing in a new crusher, determine whether the existing equipment is operating under suitable conditions.

A crusher may consume excessive electricity per ton because of poor feeding, excessive recirculation, worn components, or a downstream bottleneck.

Correcting these problems may improve performance without requiring a complete equipment replacement.

When evaluating new equipment, compare more than installed motor power.

Important considerations include actual throughput under the required conditions, finished-product gradation, energy consumption per ton, wear-part cost, maintenance requirements, and expected availability.

A higher-powered crusher may deliver a lower cost per ton if it processes substantially more acceptable material efficiently.

The appropriate decision should be based on lifecycle economics rather than motor size alone.

Frequently Asked Questions

How much electricity does a crushing plant consume per ton?

Electricity consumption varies widely depending on material hardness, feed size, final product requirements, equipment selection, and process configuration. A plant producing coarse limestone aggregate cannot be directly compared with one processing hard granite into fine manufactured sand. Actual consumption should be measured using plant electricity records and finished-product tonnage.

Which crusher is the most energy-efficient?

There is no universally most energy-efficient crusher. Jaw crushers, cone crushers, impact crushers, and other technologies are designed for different applications. The best choice depends on material properties, reduction ratio, capacity, and product specifications. Energy efficiency should be evaluated at the complete process level.

Can reducing crusher speed save electricity?

Not necessarily. Changing crusher speed may affect throughput, particle size, chamber performance, and wear. Any adjustment should remain within the manufacturer's operating limits and be evaluated against energy consumption per ton rather than instantaneous power alone.

How does screening efficiency affect crusher energy consumption?

Poor screening efficiency can cause correctly sized material to return to the crusher for unnecessary additional processing. Improving screening performance may reduce recirculating loads and increase net finished-product output.

What is the best way to reduce crushing plant operating costs?

Start by measuring actual production, energy consumption, and equipment performance. Identify major bottlenecks, improve feeding consistency, reduce unnecessary crushing, maintain equipment properly, and optimize the complete circuit. Electricity savings should be evaluated alongside wear parts, labor, maintenance, and production availability.

Conclusion

Reducing energy consumption in a crushing plant requires a system-wide approach.

Choosing suitable crushing equipment is important, but stable feeding, effective screening, controlled recirculating loads, preventive maintenance, and coordinated equipment operation can be equally valuable.

For mining and aggregate producers, the most meaningful performance indicator is often electricity consumption per ton of acceptable finished product.

By measuring this indicator and identifying where energy is being used without contributing to production, operators can make more informed decisions about process improvements and equipment upgrades.

Liming Heavy Industry provides crushing, screening, sand-making, and complete production line solutions for mining and aggregate applications. Whether developing a new plant or upgrading an existing operation, evaluating material characteristics, process flow, equipment matching, and operating costs together can help achieve more efficient and reliable production.
Previous News

14/5/2026

14/5/2026

Taming Hard Rock: A Guide to Durable and Efficient Crushing Circuits for Granite and Basalt

Processing granite and basalt—rocks with Mohs hardness of 6-7 and compressive strength often exceeding 150 MPa—demands a crushing circuit built for extreme abrasion and impact. A well-designed system balances throughput, product shape, and long-term operating costs. Here’s a practical guide based on proven industry configurations.

1. Core Challenges & Design Philosophy

  • High Abrasiveness: Rapid wear of liners and components is the primary cost driver. Equipment selection must prioritize wear resistance over initial price.

  • Impact Loads: Primary crushers must withstand repeated shock from large, hard feed.

  • Product Shape: Cubical aggregates are essential for high-value applications like concrete and asphalt; excessive flakiness reduces marketability.

  • System Stability: Consistent feed and closed-side settings (CSS) are critical to maintain throughput and product gradation.

2. Equipment Selection: The Hard-Rock Hierarchy

Stage

Recommended Equipment

Key Considerations for Granite/Basalt

Primary

Heavy-duty jaw crusher (tracked or stationary)

• Wide feed opening (≥700mm) to accept large blasted rock.
• High manganese steel or alloy liners optimized for abrasion.
• Robust frame to handle impact loads; expected liner life: 120,000–180,000 tons .

Secondary

Multi-cylinder hydraulic cone crusher

• Inter-particle compression crushing produces cubical product with low flakiness (<8%).
• Hydraulic adjustment allows real-time CSS tuning for different product specs.
• Far superior wear life vs. impact crushers on abrasive stone .

Tertiary/Shaping

Short-head cone crusher or VSI (selectively)

• Cone crusher for strict gradation control and lower wear cost.
• VSI can enhance cubicity but may incur higher wear on high-silica basalt.

Screening

3- or 4-deck vibrating screen with closed-circuit return

• 3-deck screens produce 3–4 saleable fractions + oversize return.
• 4-deck screens offer greater flexibility for tight spec products (e.g., 0–3, 3–8, 8–16, 16–22 mm) .

Feeding & Conveying

Vibrating grizzly feeder (with pre-screen) + heavy-duty conveyors

• Pre-screening removes fines to reduce wear and improve capacity.
• Steady, non-surge feeding is critical to liner life and throughput.

3. Process Flow: Proven Configurations

A. Classic Hard-Rock Closed Circuit (Most Common)

Vibrating Feeder → Jaw Crusher (Primary) → Cone Crusher (Secondary) → Screen → (Oversize return to cone)
  • Best for: 200–400 TPH plants producing standard concrete/asphalt aggregates (0–5, 5–10, 10–20, 20–31.5 mm) .

  • Why it works: Jaw handles coarse reduction; cone provides stable, shape-controlled secondary crushing; closed circuit maximizes yield and consistency.

B. Mobile “Sweet-Spot” Line (200–300 TPH)

  • Configuration: Tracked jaw + tracked cone + tracked 3‑deck screen .

  • Advantages: High mobility, fast commissioning, ideal for multi‑site contractors or quarries with moving faces.

  • Output recipes: Adjustable for road base, mixed aggregates, or premium asphalt mixes.

C. Large‑Scale Fixed Plant (600–700 TPH)

  • Flow: Jaw (PE‑1200×1500) → 2× cone crushers (HPC400) → VSI shaping → multi‑deck screening .

  • Use case: Major infrastructure projects requiring high‑volume, spec‑grade aggregates.

4. Key Design & Operational Tips

  • Capacity “Sweet Spot”: For mobile setups, 200–300 TPH offers the best balance of throughput, logistics, and flexibility .

  • Wear Management:

    • Monitor liner thickness every 250 operating hours; cone mantles typically last 450–600 hours on granite .

    • Use condition‑monitoring systems to plan replacements during scheduled downtime.

  • Dust Control: Fully enclosed conveying + centralized bag‑filter systems keep emissions below 20 mg/m³ .

  • Automation: PLC control systems monitor current, temperature, and vibration, enabling real‑time CSS adjustment and reducing changeover time by up to 80% .

  • Power Options: Diesel‑electric hybrid drives are ideal for remote hard‑rock sites without stable grid power .

5. Configuration Examples by Output Goal

Target Product

Recommended Flow

Key Equipment

Typical Capacity

Coarse aggregates (0–150 mm)

Primary only

Jaw crusher + feeder

150–250 TPH

Concrete/asphalt mixes

Jaw → Cone → 3‑deck screen

Jaw + multi‑cylinder cone + closed‑circuit screen

200–350 TPH

Premium cubical aggregates

Jaw → Cone → VSI → 4‑deck screen

Jaw + cone + shaping crusher + multi‑deck screen

250–400 TPH

High‑spec railway ballast

Closed‑circuit with precise screening

Jaw + cone + screen with strict return loop

300–500 TPH

6. Bottom Line

A durable, efficient hard‑rock circuit starts with a heavy‑duty jaw crusher for primary reduction, followed by a hydraulic cone crusher for secondary shaping—avoid impact crushers for highly abrasive granite/basalt. Closed‑circuit screening with return conveyors ensures gradation control and maximizes yield. For most quarry operators, a 200–300 TPH mobile jaw‑cone‑screen train provides the optimal blend of performance, mobility, and cost‑effectiveness . Remember: consistent feeding, proper CSS settings, and proactive wear‑part management are just as critical as equipment selection itself.

Need a tailored solution? Share your feed size, target products, and site conditions for a specific circuit recommendation.


8/5/2026

8/5/2026

How to Turn Demolished Concrete into High-Quality Recycled Aggregate

Every year, billions of tons of construction and demolition (C&D) waste are generated globally. Simply landfilling it wastes precious space, resources, and harms the environment. So, how can we transform this discarded concrete and rubble into a valuable resource? The answer lies in an efficient C&D waste crushing and screening plant.

The Core Solution: Mobile Crushing and Screening Stations

For scattered demolition sites, mobile crushing and screening stations are the ideal choice. They can be driven directly to the site, processing waste on the spot and eliminating high transport costs.

  1. Pre-Sorting and Feeding: Wood, plastic, and other impurities are removed via manual or mechanical sorting. The remaining concrete blocks are evenly fed into the crusher by a feeder.

  2. The Core Crushing Stage: A jaw crusher is typically used for primary crushing, breaking down large concrete chunks. Next, an impact crusher or cone crusher handles secondary crushing. Impact crushers produce well-shaped aggregate, ideal for road base materials. For higher demands on particle shape and hardness, a cone crusher is preferred.

  3. De-ironing and Screening: A magnetic separator removes rebar during crushing. Subsequently, a vibrating screen classifies the material into different specifications (e.g., 0-5mm, 5-10mm, 10-31.5mm), producing clean recycled coarse and fine aggregate.

  4. Final Application: This recycled aggregate can be used for road sub-bases, backfill, producing recycled bricks, concrete blocks, and even in some non-structural concrete, closing the resource loop.

The Investment Value: It not only solves waste disposal problems but also creates a new revenue stream, helps companies obtain green building certifications, and enhances their social responsibility profile.


30/4/2026

30/4/2026

Granite Crushing Plant Design for High Output

Granite is one of the hardest and most durable natural stones, widely used in construction, infrastructure, and decorative projects. Achieving high output while maintaining product quality requires a carefully designed crushing plant. This article explores the key considerations in designing a granite crushing plant that maximizes productivity, minimizes operational costs, and ensures consistent product quality.

Understanding Granite Properties

Before designing a crushing plant, it is essential to understand granite’s physical properties:

  • Hardness: Granite is extremely hard (Mohs hardness of 6–7), which affects the choice of crusher types.

  • Abrasion Resistance: High silica content can accelerate wear on crushing equipment.

  • Size and Shape: Granite blocks vary in size, influencing feeder, crusher, and conveyor selection.

Knowing these factors helps in selecting suitable crushers, screens, and conveyors that can handle high-volume operations.

Key Components of a High-Output Granite Crushing Plant

  1. Primary Crusher
    Jaw crushers or gyratory crushers are preferred for coarse crushing of granite. They provide high throughput and can handle large boulders with minimal breakdowns.

  2. Secondary Crusher
    Cone crushers or impact crushers are ideal for medium to fine crushing. They enhance product uniformity and are suitable for shaping aggregates for construction projects.

  3. Screening System
    Multi-deck vibrating screens separate crushed granite into different size fractions. Proper screening ensures consistent particle size and reduces recirculation, improving efficiency.

  4. Conveying Equipment
    Belt conveyors connect each stage of the crushing process. Efficient conveyor design minimizes material spillage and ensures smooth flow, reducing downtime.

  5. Dust and Noise Control
    Enclosures, dust collectors, and water sprays reduce environmental impact and comply with local regulations, which is particularly important in urban or sensitive areas.

Design Strategies for Maximum Output

  • Optimized Layout: Position crushers, screens, and conveyors to minimize material handling and travel distance.

  • Automated Controls: Use PLC and sensor-based systems to monitor feed rate, crusher load, and output quality. Automation reduces human error and increases throughput.

  • High-Capacity Equipment: Select crushers and screens with capacities exceeding the expected production target to accommodate peak demand.

  • Regular Maintenance: Schedule preventive maintenance for wear parts to avoid unexpected downtime and maintain consistent output.

Local Considerations for GEO Optimization

When designing a granite crushing plant, location-specific factors influence performance:

  • Availability of Granite Deposits: Proximity to quarries reduces transportation costs.

  • Local Labor and Utilities: Access to skilled operators, electricity, and water is critical.

  • Environmental Regulations: Compliance with local dust, noise, and wastewater standards ensures uninterrupted operations.

Understanding these factors helps engineers design a plant that not only achieves high output but also operates sustainably in its local environment.

Conclusion

A high-output granite crushing plant requires careful planning, robust equipment, and efficient workflows. By integrating the right crushers, screening systems, conveyors, and automation technologies, operators can maximize productivity while maintaining high-quality granite aggregates. Attention to local conditions ensures compliance and long-term operational efficiency.


24/4/2026

24/4/2026

Highlights from MiningWorld Russia 2026: A Successful Showcase in Moscow

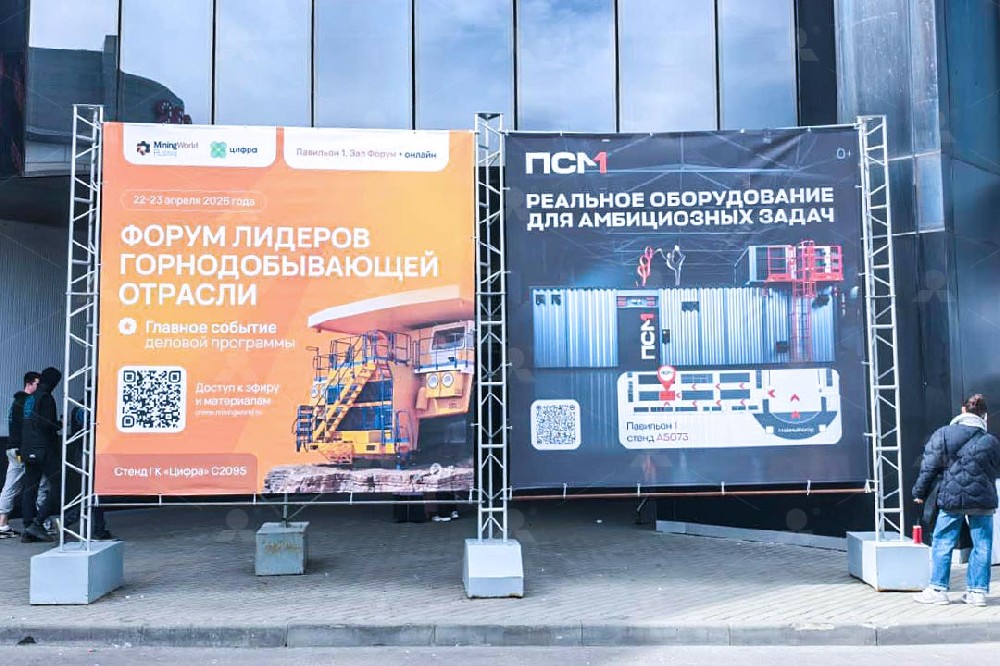
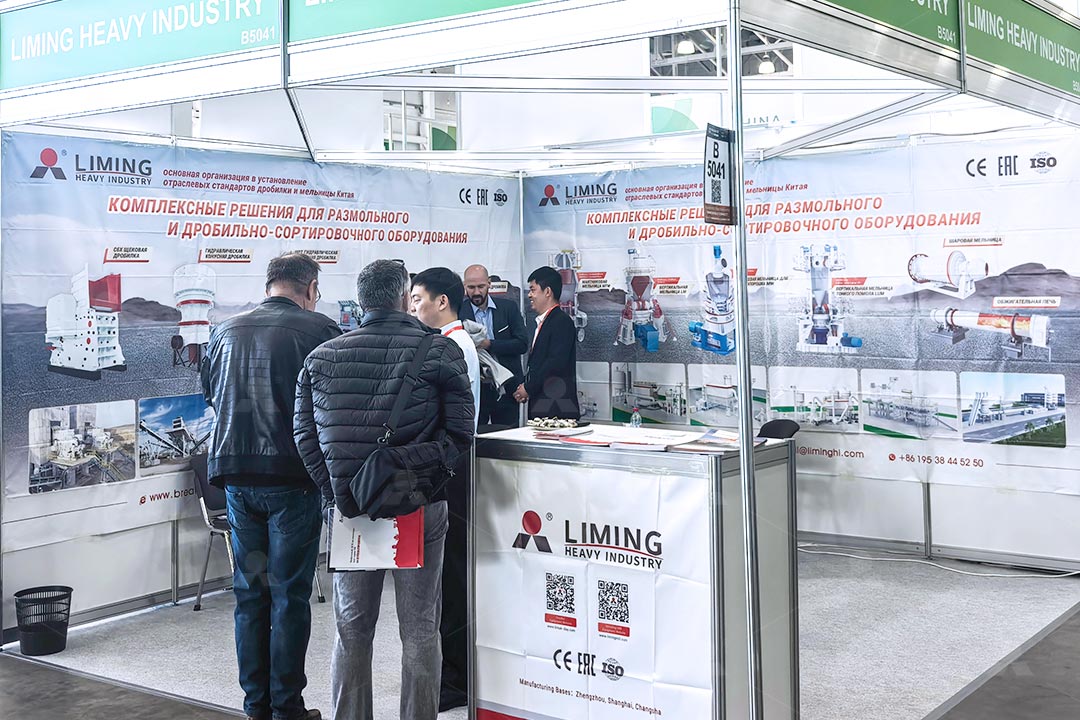
We are pleased to announce the successful conclusion of our participation in MiningWorld Russia 2026, the largest international exhibition for mining equipment, technologies, and services in Russia.

Held from April 22–24 at the Crocus Expo IEC, Pavilion 1, our team had the honor of welcoming hundreds of visitors to our booth B5041. The event provided an excellent platform to demonstrate our commitment to the mining sector and engage with key stakeholders in the industry.

Event Highlights:

  • Strong Engagement: Our technical experts held in-depth discussions with potential clients and partners regarding mining solutions.


  • Product Showcase: We displayed our core products, attracting significant interest from local mining enterprises.


  • Networking: We established valuable connections that will help us better serve the Russian market.


We are excited to share that high-resolution photos from the exhibition have just arrived! You can view the gallery [here/attached] to see the energy and excitement from our booth.

03.jpg06.jpg


Looking to Connect?

If you missed us at the show or would like to discuss business opportunities, please feel free to contact our representatives directly via WhatsApp or phone:

  • Konstantin Guo

    📱 +86 186 2558 8441


  • Sasha Du

    📱 +86 135 9883 0486


Thank you to everyone who made this event a success. We look forward to seeing you again next year!


17/4/2026

17/4/2026

Practical Ways to Reduce Operating Costs in Aggregate Crushing Plants

In today’s competitive aggregate and construction markets, profit margins are under constant pressure. While increasing production is one approach, experienced operators know that controlling operating costs is often more effective and sustainable.

Here are five proven strategies widely used in modern crushing plants.

1. Optimize the Feed Size and Gradation

Feeding oversized or uneven material into a crusher leads to:

  • Reduced efficiency

  • Increased wear

  • Higher energy consumption

Installing a proper pre-screening system can remove fine materials before crushing, allowing the crusher to focus only on what actually needs processing. This simple adjustment can improve overall efficiency by 10–15%.

2. Choose the Right Crushing Stage Configuration

A well-balanced crushing circuit reduces unnecessary load on each machine.

Typical optimized setups include:

  • Jaw + cone (for hard rock)

  • Jaw + impact (for softer materials)

  • Multi-stage crushing with screening loops

Improper configuration often results in one machine becoming a bottleneck, forcing others to operate below capacity.

3. Control Wear Parts Consumption

Wear parts are one of the largest ongoing costs in crushing operations.

To reduce replacement frequency:

  • Use the correct material grade (Mn steel, alloy, etc.)

  • Maintain consistent feed conditions

  • Avoid overloading or uneven feeding

  • Rotate liners regularly

Tracking wear life data helps predict replacement cycles and avoid emergency shutdowns.

4. Improve Automation and Monitoring

Manual operation increases the risk of human error and inconsistent performance.

Modern crushing plants increasingly use:

  • PLC control systems

  • Real-time production monitoring

  • Automatic load adjustment

These systems help maintain optimal operating conditions and reduce unnecessary energy consumption.

5. Minimize Downtime Through Preventive Maintenance

Unexpected shutdowns are often the most expensive problem.

A structured maintenance plan should include:

  • Daily inspections

  • Scheduled lubrication

  • Vibration and temperature monitoring

  • Early fault detection

Many operators underestimate how much downtime impacts profitability. In reality, even a few hours of stoppage can outweigh savings from cheaper equipment.

Conclusion

Reducing operating costs is not about cutting corners—it’s about improving efficiency at every stage of the process.

From feed control to maintenance planning, small adjustments can lead to significant savings over time. The most successful operations are those that treat cost control as a continuous process, not a one-time effort.


16/4/2026

16/4/2026

How to Choose the Right Crushing Equipment for Your Mining Project

Selecting the right crushing equipment is one of the most critical decisions in a mining project. It directly impacts production efficiency, operating costs, and long-term profitability. Yet many projects still face issues like over-investment, under-capacity, or frequent downtime—often due to poor equipment selection at the early stage.

This guide outlines the key factors that experienced operators consider before finalizing a crushing solution.

1. Understand Your Material Characteristics

Not all rocks behave the same under compression. Before choosing a crusher, you need a clear understanding of:

  • Hardness (e.g., granite vs. limestone)

  • Abrasiveness (affects wear parts consumption)

  • Moisture content (risk of clogging)

  • Feed size distribution

For example, highly abrasive materials like basalt will significantly increase liner wear in impact crushers, making jaw + cone combinations a more cost-effective choice over time.

2. Define Your Production Targets Clearly

Capacity is not just about tons per hour—it must match your actual operational conditions.

Ask yourself:

  • What is the required hourly and daily output?

  • Is production continuous or intermittent?

  • Are there peak demand periods?

A common mistake is selecting equipment based on theoretical capacity rather than real working capacity. A safety margin of 10–20% is usually recommended to handle fluctuations.

3. Determine the Final Product Requirements

End-product size and shape play a decisive role in equipment selection.

  • Coarse aggregates → Jaw crusher is sufficient

  • Medium aggregates → Cone crusher preferred

  • High-quality cubic shape (for concrete/asphalt) → Impact crusher or VSI

If your project supplies high-grade concrete, investing in shaping equipment is not optional—it directly affects your product competitiveness.

4. Consider Mobility vs. Stationary Setup

The choice between stationary and mobile crushing plants depends on project duration and site conditions.

  • Stationary plants: Suitable for long-term, high-capacity operations

  • Mobile crushers: Ideal for short-term projects, scattered sites, or urban construction

In recent years, more contractors are shifting toward mobile solutions to reduce transportation costs and improve flexibility, especially in infrastructure and demolition projects.

5. Evaluate Total Cost of Ownership (TCO)

Focusing only on initial purchase cost often leads to higher expenses later.

A proper evaluation should include:

  • Wear parts consumption

  • Energy consumption

  • Maintenance frequency

  • Downtime risk

  • Labor requirements

In many cases, a slightly higher upfront investment can reduce operating costs by 20–30% over the equipment lifecycle.

6. After-Sales Support Matters More Than You Think

Even the best equipment will require maintenance. What separates reliable suppliers from the rest is:

  • Spare parts availability

  • Technical support response time

  • Remote diagnostics capability

  • On-site service options

Delayed support can stop an entire production line—something no operator can afford.

Conclusion

Choosing the right crushing equipment is not about buying the most advanced machine—it’s about selecting a system that fits your material, production goals, and operating conditions.

A well-designed crushing solution will not only improve efficiency but also stabilize your long-term operating costs and reduce unexpected risks.


10/4/2026

10/4/2026

How to Lower Wear Parts Cost in Aggregate Plants

In aggregate production, wear parts are one of the most significant ongoing operating costs. Components such as jaw plates, cone liners, mantles, blow bars, and screen media are constantly exposed to impact, abrasion, and high-pressure loads. If not properly managed, frequent replacements can increase downtime, raise cost per ton, and reduce overall plant profitability.

The good news is that wear parts cost can be significantly reduced through proper equipment selection, optimized process design, and disciplined maintenance practices.

This article outlines practical strategies to lower wear parts costs in aggregate plants while maintaining stable output and high product quality.


1. Match the Right Equipment to the Material

One of the most common reasons for excessive wear is using equipment that is not suitable for the material.

Material-based recommendations:

  • Granite / Basalt / Hard rock
    → Jaw crusher + cone crusher
    → Avoid excessive impact crushing

  • Limestone / Soft to medium-hard rock
    → Jaw crusher + impact crusher or cone crusher

  • River stone / Abrasive aggregate
    → Compression crushing + VSI shaping (if needed)

Using the correct crusher type reduces unnecessary impact stress and extends wear part life.


2. Control Feed Size and Gradation

Improper feed conditions accelerate wear and reduce crushing efficiency.

Common problems:

  • Oversized rocks entering the crusher

  • Excessive fines causing packing

  • Uneven feed distribution

Solutions:

  • Install vibrating feeders with grizzly bars

  • Pre-screen fines before crushing

  • Maintain consistent feed size

Stable feed conditions ensure smoother crushing and more uniform liner wear.


3. Optimize Crusher Settings

Incorrect crusher settings can dramatically increase wear.

Key settings to monitor:

  • Closed Side Setting (CSS)
    Overly tight CSS increases pressure and liner wear

  • Chamber profile
    Wrong chamber design causes uneven wear

  • Crusher speed
    Excessive speed may increase abrasion

Best practice:

Adjust crusher settings based on:

  • Material hardness

  • Feed size

  • Target output

Optimized settings improve both wear life and production efficiency.


4. Improve Material Flow and Plant Layout

Poor plant layout can create bottlenecks and recirculation overload, which increase wear.

Common issues:

  • Frequent crusher overload

  • Excessive recirculating load

  • Material buildup at transfer points

Solutions:

  • Balance crusher and screen capacities

  • Improve transfer chute design

  • Use closed-circuit systems

A smooth material flow reduces unnecessary crushing cycles and wear.


5. Select High-Quality Wear Materials

Wear parts material selection has a major impact on service life.

Common wear materials:

  • High manganese steel

  • Alloy steel

  • Chrome alloys

  • Composite wear materials

Selection depends on:

  • Material hardness

  • Abrasiveness

  • Impact load

High-quality wear parts may cost more initially but often reduce total replacement frequency and downtime.


6. Implement Preventive Maintenance

Wear part management should be proactive, not reactive.

Key maintenance actions:

  • Inspect wear thickness regularly

  • Rotate liners if applicable

  • Check bolt tightness

  • Monitor vibration and noise

  • Maintain lubrication systems

A preventive maintenance plan helps detect wear issues early and avoid major failures.


7. Train Operators for Correct Crusher Operation

Operator practices directly affect wear part consumption.

Common mistakes:

  • Overfeeding

  • Uneven loading

  • Ignoring warning signs

Benefits of training:

  • Better feed control

  • Timely adjustments

  • Safer operation

Well-trained operators can significantly reduce wear-related costs.


8. Use Automation and Monitoring Systems

Modern aggregate plants increasingly use automation to optimize performance.

Useful technologies:

  • Load monitoring

  • CSS automatic adjustment

  • Wear tracking sensors

  • Predictive maintenance alerts

Automation improves consistency and helps avoid conditions that accelerate wear.


Conclusion

Lowering wear parts cost in aggregate plants requires a combination of the right equipment, optimized crushing conditions, quality wear materials, and disciplined maintenance. By improving material flow, feed control, and operator practices, aggregate producers can significantly reduce cost per ton and improve plant profitability.

A strategic approach to wear management not only saves money but also ensures more stable, efficient, and sustainable production.


2/4/2026

2/4/2026

Common Jaw Crusher Problems and How to Fix Them

Jaw crushers are widely used in mining, quarrying, and construction industries due to their reliability and high crushing efficiency. However, like any heavy-duty equipment, they can encounter operational issues that affect productivity, increase downtime, and raise maintenance costs.

In this guide, we’ll explore the most common jaw crusher problems, their causes, and practical solutions to keep your equipment running smoothly.


1. Uneven Output Size

Problem:

The crushed material size is inconsistent, with too many oversized particles.

Causes:

  • Worn or uneven jaw plates

  • Improper discharge opening setting

  • Uneven feeding

Solutions:

  • Regularly inspect and replace jaw plates

  • Adjust the discharge opening according to production requirements

  • Ensure consistent and uniform feeding using a vibrating feeder


2. Low Crushing Efficiency

Problem:

The crusher output is lower than expected, affecting overall production capacity.

Causes:

  • Insufficient motor power

  • Incorrect speed or improper pulley configuration

  • Excessive material hardness or moisture

Solutions:

  • Check motor performance and electrical supply

  • Optimize pulley and speed settings

  • Pre-screen wet or sticky materials before crushing


3. Excessive Vibration

Problem:

The machine vibrates abnormally during operation, which can damage components.

Causes:

  • Loose foundation bolts

  • Uneven installation or unstable base

  • Worn bearings

Solutions:

  • Tighten all foundation and frame bolts

  • Re-level and stabilize the installation base

  • Replace worn bearings promptly


4. Jaw Plate Wear Too Fast

Problem:

Jaw plates wear out quickly, increasing operating costs.

Causes:

  • High abrasiveness of materials

  • Incorrect material feeding method

  • Poor quality jaw plates

Solutions:

  • Use high-quality, wear-resistant jaw plates

  • Avoid feeding oversized or uneven materials

  • Optimize feed distribution across the crushing chamber


5. Bearing Overheating

Problem:

Bearing temperature rises abnormally, potentially leading to failure.

Causes:

  • Insufficient lubrication

  • Contaminated lubricant

  • Excessive load or improper installation

Solutions:

  • Regularly lubricate bearings with appropriate grease

  • Keep lubrication systems clean

  • Monitor load and ensure proper alignment


6. Blockage in Crushing Chamber

Problem:

Material gets stuck in the crushing chamber, causing downtime.

Causes:

  • Wet or sticky materials

  • Overfeeding

  • Narrow discharge opening

Solutions:

  • Reduce feed rate and maintain steady feeding

  • Use pre-screening equipment for wet materials

  • Adjust discharge opening properly


7. Abnormal Noise

Problem:

Unusual noises during operation indicate potential internal issues.

Causes:

  • Loose components

  • Damaged toggle plate

  • Worn internal parts

Solutions:

  • Inspect and tighten all components

  • Replace damaged toggle plates

  • Conduct routine maintenance checks


Preventive Maintenance Tips

To minimize jaw crusher problems and extend equipment lifespan:

  • Perform regular inspections and scheduled maintenance

  • Keep a proper lubrication routine

  • Train operators for correct usage

  • Maintain stable and continuous feeding

  • Use genuine spare parts


Conclusion

Understanding common jaw crusher problems and their solutions is essential for maintaining high efficiency and reducing operational costs. By addressing issues early and implementing preventive maintenance strategies, you can significantly improve equipment performance and longevity.

If you're experiencing frequent breakdowns or planning to upgrade your crushing equipment, professional technical support can help you optimize your production line.


  • Home
  • Prev
  • ···34567···
  • Last
Clicky